A buyer receives two shipments of the same walnut-finish cat tree, three months apart: the first a warm chocolate brown, the second noticeably lighter with one perch visibly grayer. Nothing is “defective” — but the showroom display looks mismatched and the review photos won’t match the product photos. Wood color consistency in production separates a factory that makes furniture from one that makes a brand’s furniture.
Wood Color Consistency in Production: Why Does Tone Drift Between Runs?
Wood color consistency in production means parts made months apart — different lumber lots, finish batches, operators — still read as the same product. Tone drifts because wood is natural: heartwood and sapwood differ in color, mineral content varies by region, finish absorption changes with grain density. Add inconsistent coating mixes or rushed curing, and drift becomes visible.
The buyer’s risk: mismatched pieces in one carton trigger “not as described” complaints even when dimensions and structure are perfect. Color drift is a quality failure even when nothing is broken. Factories that control it treat color as an engineering parameter, with control points at material selection, grading, finishing, and inspection.
Same-Batch Material Selection: the First Control Point
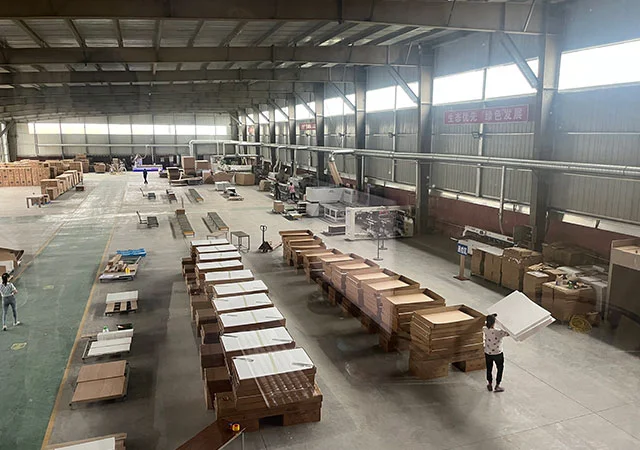
Consistency starts before the first cut. A cheap factory mixes boards from three suppliers and hopes; a professional factory buys kiln-dried lumber to a moisture spec, then grades and stages boards by tone — so parts that will sit side by side started as neighbors in the same stack.
| Control Point | Méthode | Détail |
|---|---|---|
| Moisture | Kiln-dried stock at 8–12% | Prevents post-finish tone shift |
| Tone grouping | Sort boards by tone | Matched boards go into one product |
| End-grain seal | Seal lumber ends in storage | Prevents uptake that darkens end grain |
| Heart/sapwood | Separate or blend deliberately | Unplanned mixes create visible patches |
The cheapest place to control color is the lumber rack, not the spray booth. Auditing a factory? Look at the staging area: boards grouped by tone signal a factory that takes consistency seriously. Our 5 wood species for premium pet furniture breakdown covers how species affects natural variation.
Grading and Staging: Keeping Tones Together Before Cutting
Material selection is only the first half; the factory must keep matched boards together through cutting. In our workshop, the grader marks tone groups with chalk codes, and cut lists keep all visible parts of one unit — perch, post sleeves, base trim — in the same tone group. Offcuts from a darker board never drift into a light unit’s bin.
This discipline fails where the cutting team is measured on speed alone. A cutter who grabs the nearest board saves thirty seconds and costs the factory a color complaint three months later. It also protects against a subtler problem: different boards absorb stain differently, so identical finish formulas produce different tones on unmatched wood. Consistent input, consistent output.
Finish Formulation Records: the Recipe for Wood Color Consistency
The finish booth is where small variations become visible: water-based coatings react to mix ratios, application passes, and drying — a second coat before the first has flashed off darkens the tone. Professional factories treat the finish like a recipe: every formulation recorded, every run follows the record.
| Record Field | What to Record | Pourquoi c'est important |
|---|---|---|
| Coating | Exact product and version | The record pins the formulation actually used |
| Mix ratio | Pigment/toner to base by weight | Eyeballed ratios drift fastest |
| Application | Coat count, gun settings | Film thickness shifts tone |
| Flash-off/dry | Minutes between coats, cure conditions | Rushed coats darken the finish |
| Batch code | Linked to the run | Traceability for complaints |
If the factory cannot show the finish record for your last run, it cannot promise the next run will match. Ask for formulation records like test reports — the same kind of evidence. Our guide des finitions de bois sans danger pour les animaux de compagnie explains the coating types.
IPQC Color-Board Comparison: the Gate Between Batches
Even with matched lumber and recorded formulations, the factory needs a physical gate: the master color board — a buyer-approved reference kept under controlled conditions. During production, IPQC compares live parts against it under standardized lighting; off-tolerance parts don’t move to packing.
| Step | Méthode | Détail |
|---|---|---|
| Master board | Buyer-signed reference part | The single source of truth for tone |
| Lighting | D65 daylight lamps, neutral booth | Warm fluorescents hide tone differences |
| Check frequency | Each shift start, each material change | Drift caught at the first part |
| Deviation action | Hold, reformulate, re-approve | Off-tone parts never ship “close enough” |
On our line, the IPQC inspector holds each first-article part against the master board under the viewing lamp before release — a two-minute ritual that has caught formulation errors before they filled a container. The color board is the cheapest insurance in the factory.
One trap: some “color problems” aren’t color problems at all — a part matching under D65 lamps can look different under warm showroom spots, and phone flash creates tones the factory never produced. Specify viewing conditions (D65, 45° angle) in the quality agreement. A factory that argues about color under random warehouse fluorescents is negotiating with a blindfold on. Notre inspection de qualité des meubles pour animaux de compagnie guide covers viewing conditions in the broader routine.
The Limits of Color Consistency in Natural Wood
Honesty requires the other side: perfect color uniformity is unachievable in solid wood, and any factory promising it is selling fiction. Growth rings, mineral streaks, the heartwood-to-sapwood gradient — that’s the material’s character, the reason solid wood is desirable. What a factory can promise is controlled consistency: matched tone groups, recorded formulations, inspection gates within an agreed band.
Your choices set the difficulty: dark stains and opaque finishes hide variation; clear, light natural finishes expose it. The lighter and clearer the finish, the tighter the factory’s material discipline must be — worth asking when a supplier quotes identical terms for natural oak and dark walnut. Certified lumber varies by region, which is why Certification FSC belongs in the color conversation, alongside Conformité au titre VI de la TSCA de l'EPA compliance for composite components.
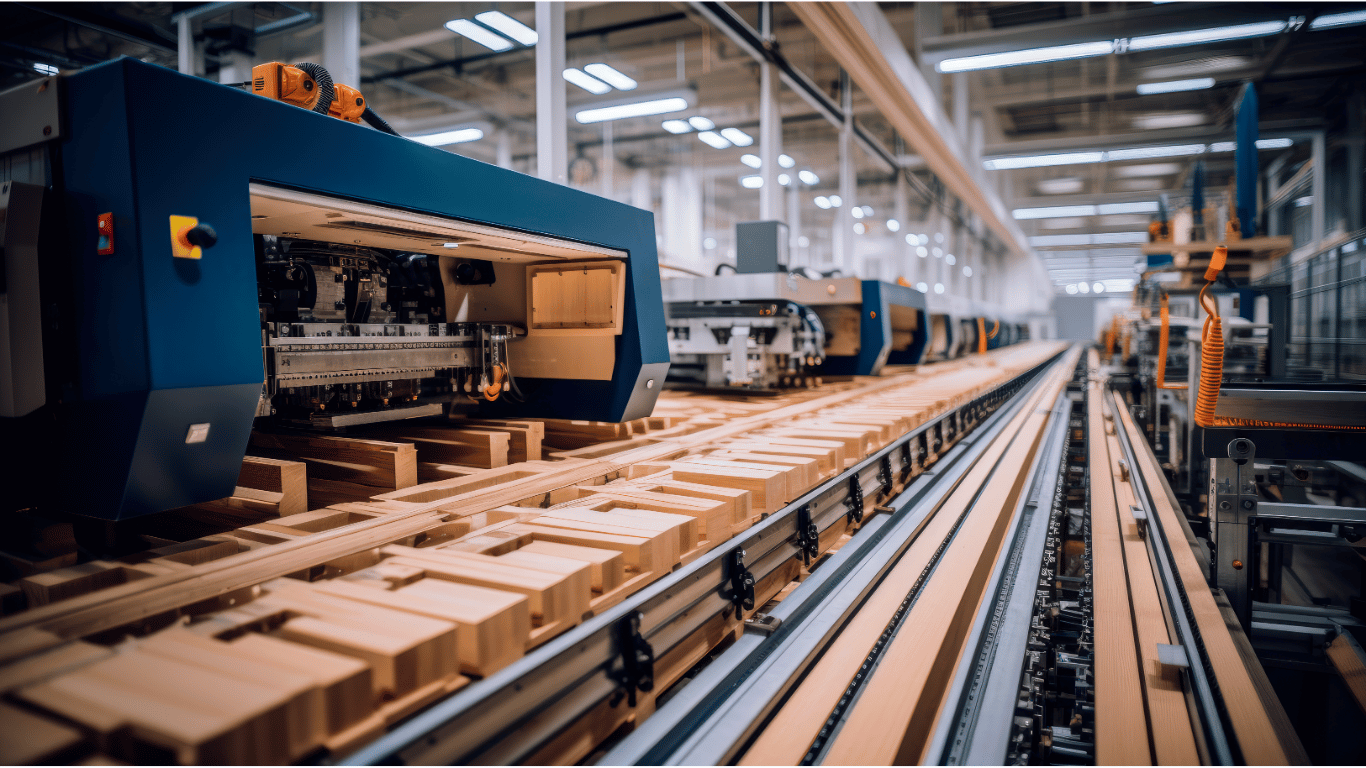
voir notre atelier où les meubles pour chats en bois massif sont usinés et assemblés. Watch how color consistency is controlled on a real production line.
How Solid Pet Wood Controls Wood Color Consistency
Color control at Solid Pet Wood is a chain, not a checkpoint: tone-grouped kiln-dried stock at the lumber rack, chalk-coded cut lists, recorded finish formulations, and the IPQC color-board gate where each run’s first articles meet your approved master board under D65 lighting.
A cheap factory hopes the color matches. A professional factory builds the match into the process. For private label buyers, that’s what protects your product photography, showroom displays, and review ratings across reorders months apart. If consistent tone matters to your brand, pour un examen d'ingénierie avant l'outillage. and ask about our wood color consistency controls.
FAQ
What causes wood color drift between production runs?
Different lumber lots (heartwood vs sapwood, growing regions), inconsistent finish mix ratios, rushed curing, and unmatched boards in the same product. Each factor is small alone; together they produce visible tone differences.
How do factories control wood color consistency?
Through a chain of control points: tone-grouped kiln-dried lumber, chalk-coded cut lists, recorded finish formulations, and IPQC comparison against a buyer-approved master color board under standardized lighting.
What is a master color board?
A buyer-approved reference part kept under controlled conditions — the single source of truth for correct tone. Parts beyond tolerance don’t ship.
Why do parts match in the factory but look different in the showroom?
Lighting. Parts matching under D65 lamps can look different under warm showroom spots or phone flash. Specify viewing conditions (D65, 45° angle) in the quality agreement so both sides judge tone under the same light.
Can solid wood ever have perfectly uniform color?
No — growth rings, mineral streaks, and the heartwood-to-sapwood gradient are the material’s character. What a factory can promise is controlled consistency: matched tone groups, recorded formulations, inspection gates keeping variation within an agreed band.
Does finish choice affect how hard color control is?
Yes. Dark stains and opaque finishes hide variation; clear, light natural finishes expose it. The lighter and clearer the finish, the tighter the factory’s material discipline — a useful question when comparing quotes.
Support OEM/ODM
Besoin d'un plan de production personnalisé pour un arbre à chat ?
Envoyez des photos de référence, les dimensions cibles, les préférences de matériaux, les besoins en emballage et la direction du marché. Nous pouvons examiner la faisabilité, l'échantillonnage, les MOQ et l'emballage d'exportation avant la production. Demander un devis OEMLignes de produits associées
Explorez les meubles pour chats en bois que nous pouvons fabriquer.
Guides d'achat associés